GB/T 44678-2024 MARINE CRYOGENIC CHECK VALVES
Item | Description |
|---|---|
Product Name | GB/T 44678-2024 MARINE CRYOGENIC CHECK VALVES |
Certificates | ABS, LR, BV, DNV, RINA, CCS |
FOB Price | Get Latest Price Now |
Warranty | 12 months (unless otherwise specified) |
Place of Origin | China |
Overview
KEY FEATURES
Standard: GB/T 44678-2024 / ISO 20602:2019
Application: Ultra-low temperature (-196°C to -50°C)
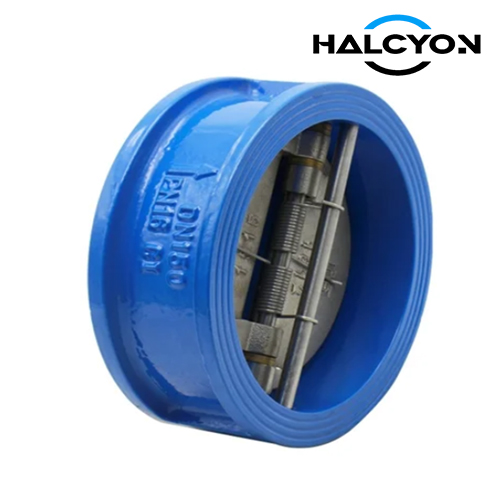
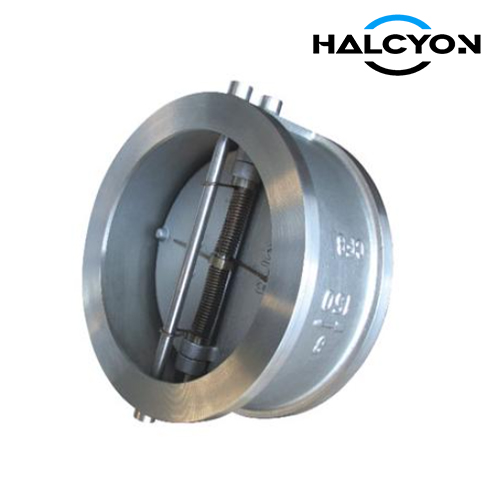
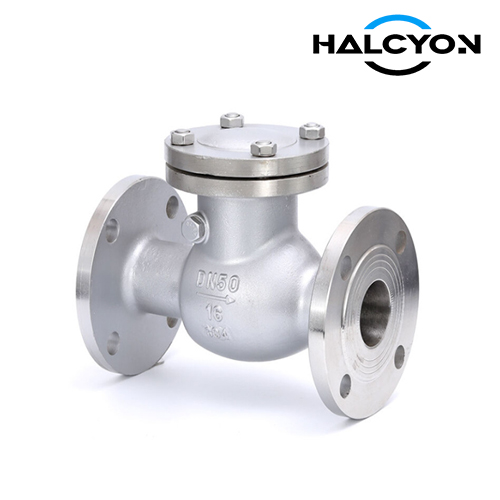
Structure Type: Lift Type or Dual-plate Swing Type
Design Temperature Range: -196°C to +100°C
Manufacturing Methods: Forged or Cast
Surface Treatment: Pickling and Passivation
Inspection Standard: API 598, ASME B16.34
1. MEDIA TYPES AND PRESSURE-TEMPERATURE RATINGS
TABLE 1 - MEDIA TYPES
| MEDIA TYPE | TEMPERATURE (BAR) / °C | DENSITY / (kg/m³) |
|---|---|---|
| LNG (Liquefied Natural Gas) | -165 ~ -80 | 430 ~ 470 |
| NG (Natural Gas) | -160 ~ -65 | 0.7 ~ 0.89 |
| LN2 (Liquid Nitrogen) | -196 | 801 |
| N2 (Nitrogen) | -196 ~ -65 | 4.188 |
TABLE 2 - WORKING PRESSURE AND DESIGN TEMPERATURE
| PN | Class | MAXIMUM WORKING PRESSURE MPa | REMARKS |
|---|---|---|---|
| 20 | 150 | 2.0 | Ambient Temperature |
| 50 | 300 | 5.2 | Ambient Temperature |
| 110 | 600 | 10.3 | Ambient Temperature |
| 150 | 900 | 13.8 | Ambient Temperature |
| 250 | 1500 | 15.5 | Ambient Temperature |
Note: Pressure ratings correspond to ASME B16.34. Design temperature shall be between -196°C and 100°C. When the pressure class exceeds Class900, it may be agreed upon by both parties. Working pressure depends on the purchaser's piping system.
2. DESIGN AND CONSTRUCTION
2.1 BASIC STRUCTURE
The check valve shall be of the lift type or dual-plate swing type. The function and standardization requirements shall comply with relevant standards. If the structure differs, the manufacturer and purchaser must reach an agreement.
2.2 BODY
Type: Straight-through type.
Material: Performance shall not be lower than those specified in Table 3. For flanged end types, welded end materials may be used as substitutes.
Manufacturing:
Structural length shall comply with API 594 or ASME B16.10.
Minimum body wall thickness shall comply with ASME B16.34.
Butt-welding ends: Shall comply with ASME B16.25.
Flanged ends: NPS24 (DN600) and below shall comply with ASME B16.5. PN20 and PN50 (Class150 & Class300) shall use raised face (RF) flanges; PN110 (Class600) and above shall use large tongue (LGF) flanges or raised face (RF) flanges, complying with ASME B16.5 and ASME B16.47.
2.3 DISC
Type: When the disc and seat are connected by a threaded type, it shall be fixed with a set screw before welding.
Material: ASTM A182 F316, ASTM A351 CF8M, or better. To improve wear resistance, the sealing surface shall be surface-hardened with a minimum thickness of 1.6 mm.
2.4 SEAT
Type: The seat may be a solid type (single-piece) or a two-piece type.
Material: ASTM A182 F316, ASTM A351 CF8M, or better. To improve wear resistance, the sealing surface shall be surface-hardened with a minimum thickness of 1.6 mm.
2.5 GASKET
Materials suitable for continuous operation at -196°C to +100°C shall be used.
2.6 BOLTS AND NUTS
Design: Bolts and nuts for the bonnet flange shall comply with BS 1868.
Material: Bolts shall not be lower than ASTM A320 Gr. B8; Nuts shall not be lower than ASTM A194 Gr. 8.
3. MATERIALS OF MAIN PARTS
TABLE 3 - MATERIALS FOR MANUFACTURING METHODS
| MANUFACTURING METHOD | FLANGED END TYPE | WELDING END TYPE |
|---|---|---|
| Forged | ASTM A182 F304, F316 | ASTM A182 F304L, F316L |
| Cast | ASTM A351 CF8, CF8M | ASTM A351 CF3, CF3M |
Note: Other materials may be used provided they are equivalent to or better than the specified materials in terms of manufacturing process, mechanical properties, and corrosion resistance.
4. TESTING, INSPECTION AND NDT REQUIREMENTS
4.1 MATERIAL INSPECTION
Chemical composition, mechanical properties, and low-temperature impact tests shall be conducted on main parts.
Impact Test: At -196°C, the minimum lateral expansion of 3 specimens shall be greater than 0.381 mm. The ferrite content in austenitic stainless steel shall be between 5% and 10%.
4.2 NON-DESTRUCTIVE TESTING (NDT)
Radiographic Testing (RT): Weld seams shall be 100% RT. Acceptance criteria per ASME B16.34 and MSS SP-55.
Penetrant Testing (PT): Per ASME BPVC Sec. V Art. 6.
Ultrasonic Testing (UT): Per ASME BPVC Sec. V Art. 4.
4.3 WELDING AND HEAT TREATMENT
Welding shall be performed according to qualified WPS/PQR. NDT of welds shall be agreed upon by both parties.
Heat treatment shall be agreed upon by both parties.
4.4 SURFACE TREATMENT
All surfaces of the valve shall be pickled and passivated.
5. INQUIRY REQUIREMENTS (FOR BUYERS)
To ensure an accurate quotation and compliance with GB/T 44678-2024 / ISO 20602:2019, please provide the following details:
Product Name: Marine Cryogenic Check Valve
Standard: GB/T 44678-2024 / ISO 20602:2019
Nominal Diameter (DN/NPS): [e.g., 25, 50, 100]
Nominal Pressure (PN/Class): [e.g., PN20 (Class150), PN50 (Class300)]
Working Medium: [e.g., LNG, NG, LN2, N2]
Design Temperature: [e.g., -196°C]
End Connection: [ ] Flanged (RF/LGF) / [ ] Butt-welding
Body Material & Manufacturing Method: [ ] Forged (ASTM A182 F304/F316/L) / [ ] Cast (ASTM A351 CF8/CF8M/CF3/CF3M)
Valve Structure Type: [ ] Lift Type / [ ] Dual-plate Swing Type
Classification Society Required: [e.g., NK, LR, DNV, ABS, CCS, or None]
Quantity: [e.g., 10 pcs]
Destination Port: [e.g., Singapore, Rotterdam]
Inspection Requirements: [e.g., EN 10204 3.1 Certificate, Third-Party Witness]